

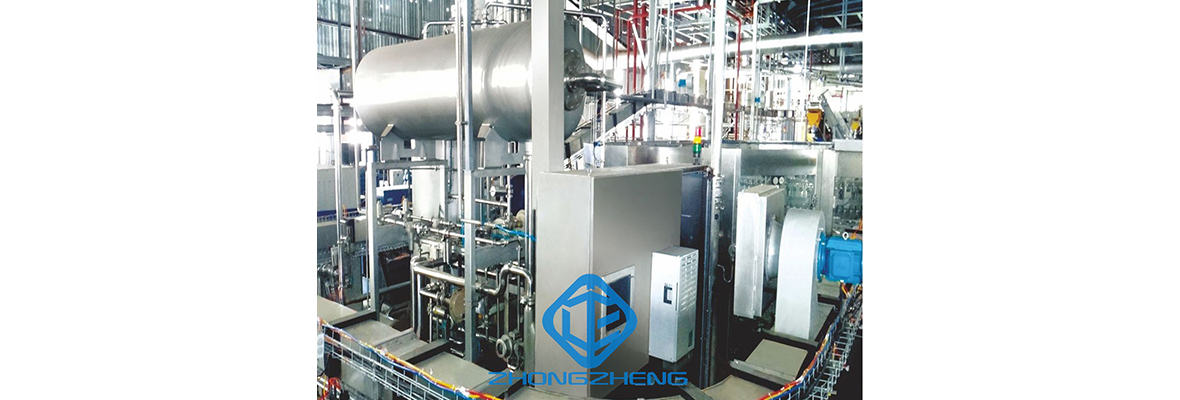
CO₂ Beverage Mixer
This integrated CO₂ beverage mixer is purpose-built for carbonated soft drinks, sparkling water and other carbonated beverage production lines. It combines a vacuum deaerator, CO₂ injector, plate heat exchanger, finished product tank, optional inline CO₂ and Brix detector, machine frame and electrical control cabinet into one compact, self-contained system. A fully automatic control architecture features independent control loops for pressure, liquid level, temperature, Brix, gas volume and all other critical operating parameters, enabling consistent, unattended production operation.
High-Efficiency Deaeration
Dissolved air is displaced by CO₂ before water enters the deaeration tank. Specialized nozzles disperse the liquid into high-velocity water mist to maximize gas-liquid contact surface area, delivering a deaeration performance of 0.94 bar or higher. A dual-stage deaeration configuration is available as an upgrade for applications with stricter oxygen removal requirements.
High-Precision Brix Control
The inline water-syrup blending system consists of a water pump, water mass flow meter, syrup pump, syrup mass flow meter and syrup control valve, all governed by a dedicated closed-loop controller. This setup achieves Brix control accuracy of ±0.05 °Brix or better, ensuring uniform sweetness and flavor consistency across every production run.
Stable, Accurate Carbonation
Beverage gas volume (GV) is fully adjustable inline, with a control accuracy of ±0.10 GV or better based on a preset 4.2 GV baseline. The system maintains consistent carbonation levels even during line speed fluctuations and product changeovers.
Reduced Production Waste
Engineered to minimize material loss, the system drastically cuts syrup waste during production start-ups and format changeovers, lowering operational costs for high-volume production facilities.
Optional inline Brix and CO₂ meters are available for real-time process monitoring and full production traceability.
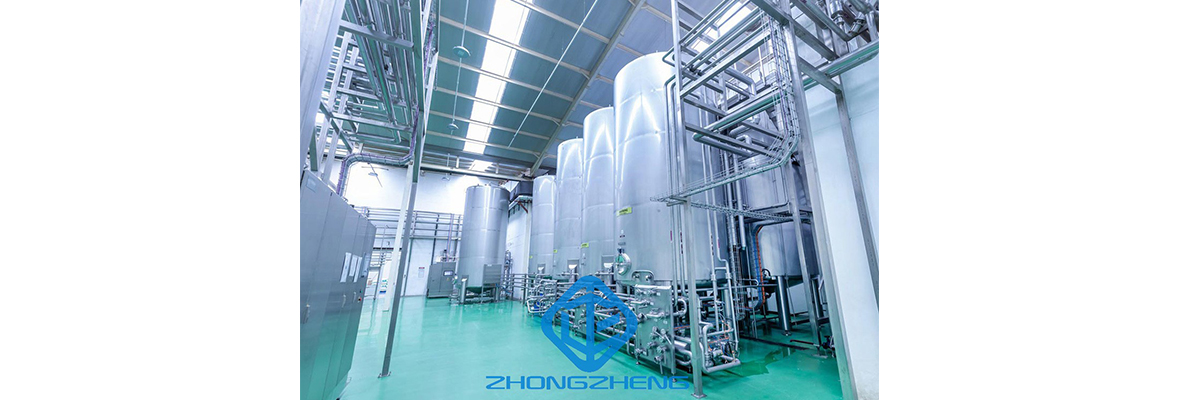
Beverage Syrup Processing System
Good to know
Our syrup processing systems cover the full spectrum of beverage syrup preparation workflows, from sugar dissolvers and syrup flash pasteurizers to batch mixing systems, mixing tanks and precision syrup production lines. We deliver custom-engineered syrup room solutions tailored to each customer’s unique operational requirements. These systems reliably produce carbonated and non-carbonated beverages, fruit juices, drink syrups, soda drinks, juice spritzers, mixed alcoholic beverages and energy drinks.
Well thought out
Recipe-controlled production in the syrup room, paired with optimized shortest-path conveying routes, reduces long-term product waste and material loss. Centralized recipe management and beverage-specific processing protocols ensure consistent, high-quality output across every production run. For fully integrated production lines, the entire syrup processing system can also be fully automated with seamless upstream and downstream integration.
Convincing
-Versatile design suitable for a wide range of beverage and syrup production applications
-Optimized production of both finished beverages and semi-finished syrups for further processing, including products containing fruit pieces and fibers
-Tailor-made system configurations built to meet individual customer production requirements
Sustainable
-Minimizes long-term product loss through recipe-controlled production and optimized short conveying routes
-High heat recovery rates reduce overall energy consumption and operational costs
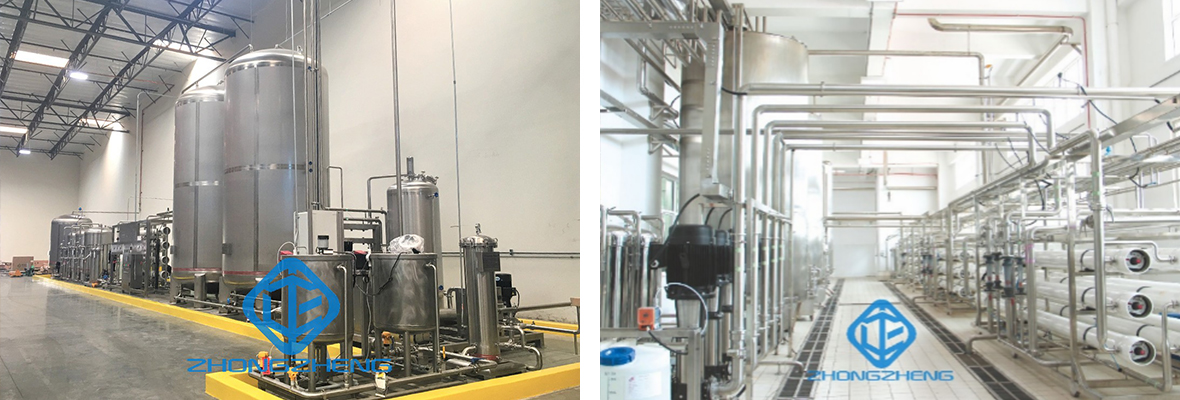
R.O. Water treatment
One stage R.O. Water treatment
Raw Water Tank→ Raw Water Pump→ Quartz Sand Filter→ Activated Carbon Filter→ 5 Micron Filter→ 1 Micron Filter→ High Pressure Pump→ Primary Reverse Osmosis Device→ Intermediate Water Tank→ Booster Pump→ Ozone Mixer→ Pure Water Pump→ Pure Water Tank→ External Supply Pump→ Titanium Tube Filter→ External Supply→ To Filling
Two stage R.O. Water treatment
Raw Water Tank→ Raw Water Pump→ Quartz Sand Filter→ Activated Carbon Filter→ 5 Micron Filter→1 Micron Filter→ High Pressure Pump→ Primary Reverse Osmosis Device→Intermediate Water Tank→ Booster Pump→ Secondary High Pressure Pump→ Secondary Reverse Osmosis Device→ Ozone Mixer→ Pure Water Pump→ Pure Water Tank→ External Supply Pump→ Titanium Tube Filter→ External Supply→ To Filling

Can Sweep-Off Depalletizer
This heavy-duty sweep-off can depalletizer is purpose-built for automated layer-by-layer depalletizing of aluminum and tin beverage cans. Its signature high-level discharge design delivers intact can layers directly to elevated line conveyors, making it a reliable feeding solution for high-speed can filling, seaming and downstream packaging lines across the beverage industry.
High-Level Discharge Transfer Mechanism
Engineered to align with higher-positioned production conveyors, the high-level discharge system transfers full layers of cans via a smooth horizontal sweep motion, instead of the vertical drops used in conventional gravity-fed depalletizers. This gentle sweep-off action moves entire can layers in one uniform, controlled movement, eliminating impact shocks that commonly cause can tipping, body scuffing, print damage or denting. By maintaining precise can alignment throughout the transfer, the system ensures a steady, uninterrupted can feed to downstream processes while preserving full product and packaging integrity.
Broad Can Format & Line Compatibility
The depalletizer supports all standard beverage can formats, including 202 standard cans and sleek cans, for applications such as carbonated soft drinks, beer, fruit juice, energy drinks and ready-to-drink beverages. It can be customized to match specific line layouts, conveyor heights and production throughput requirements, and integrates seamlessly with upstream pallet handling equipment and downstream filling and sealing systems to create a fully automated end-to-end can production flow.
Reliable, Low-Maintenance Industrial Performance
Built for continuous round-the-clock production environments, the system features a robust heavy-duty steel frame and precision-machined sweep mechanism for long-term, repeatable performance. Fully automated operation reduces reliance on manual material handling, lowering labor costs and reducing the risk of workplace injury. The simple, proven mechanical design also minimizes routine maintenance requirements and supports extended production runs with minimal unplanned downtime.


Mechanical Can Filling System
This mechanical can filling system features a proven mechanical filling valve design, purpose-built for canned carbonated beverages, beer and energy drink production. It delivers a rated capacity of 4,000 to 20,000 cans per hour (CPH) based on 500ml containers, suited for mid-volume beverage manufacturing lines.
-Time-tested mechanical valve structure optimized for carbonated beverage filling
-Simple, durable design with low operational complexity and maintenance costs
-Compatible with standard aluminum and tinplate beverage cans across mainstream sparkling drink, beer and energy drink applications


Shrink Sleeve Labeling Machine
This shrink sleeve labeling machine is built for canned drinking water, juice, carbonated soft drinks and other beverage products. It delivers a rated production capacity of 6,000 to 24,000 cans per hour (CPH) based on 500ml containers, with support for sizes up to 2,000ml.
-Optional dedicated sleeve supply unit available, tailored for high-throughput production lines and low-labor operation needs
-Reliable label positioning for uniform, consistent packaging results
-Seamless integration with upstream filling lines and downstream shrink tunnels


Bottle conveyor system, Pack conveyor system, Pallet conveyor system is suitable for bottled drinking water, juice, carbonated soft drinks etc. with production capacity from 4000BPH to 60000BPH based on 500ml. Up to 2000ml.
Good to know
Processes which are matched to one another like clockwork are the be-all and end-all of beverage filling. Transportation and conveying equipment plays a particularly important role here - after all, it is responsible for making a functioning, perfectly matched system from a collection of individual machines. The conveyor actively helps in transporting products and placing them in magazines with pinpoint accuracy. As well as non-returnable and returnable packaging such as plastic crates and returnable plastic displays, you can also convey cartons, trays and foil packs reliably to their destination. In addition, the decentralized control components ensure that you can control and regulate every single conveyor segment separately. As a result, the frequency-controlled drives adapt themselves perfectly to the particular operating state of your machine, thus enabling soft deceleration and jerk-free conveying which is gentle on the packaging.
Well thought out
The integrated speed control ensures minimum product wear while at the same time providing optimum machine performance. As well as the individual adaptation options afforded by its modular system, it simultaneously forms the basis of a safe and controlled throughput of your product streams. In addition, special attention has been paid in the design to its hygienic advantages. All segments of the conveyor system are made from stainless steel or other non-rusting material, which results in particularly long life and hygienic advantages. In addition, the automatic railing adjustment ensures short changeover times and therefore high system efficiency.
Convincing
Sustainable
